Skip to content

If a problem isn't visible, it doesn't get fixed.

I have spent thirty years in the commercial and special vehicle and agricultural machinery industries, working on the assembly line and in quality, product development, technical service and supply chain. Over those years I learned to tackle problems from the same starting point every time: first you have to see them clearly, then you can look for the cause. AndonLab is the name I gave to this way of working.

30 years
Assembly line,
Iveco Suzzara
Board of
Directors
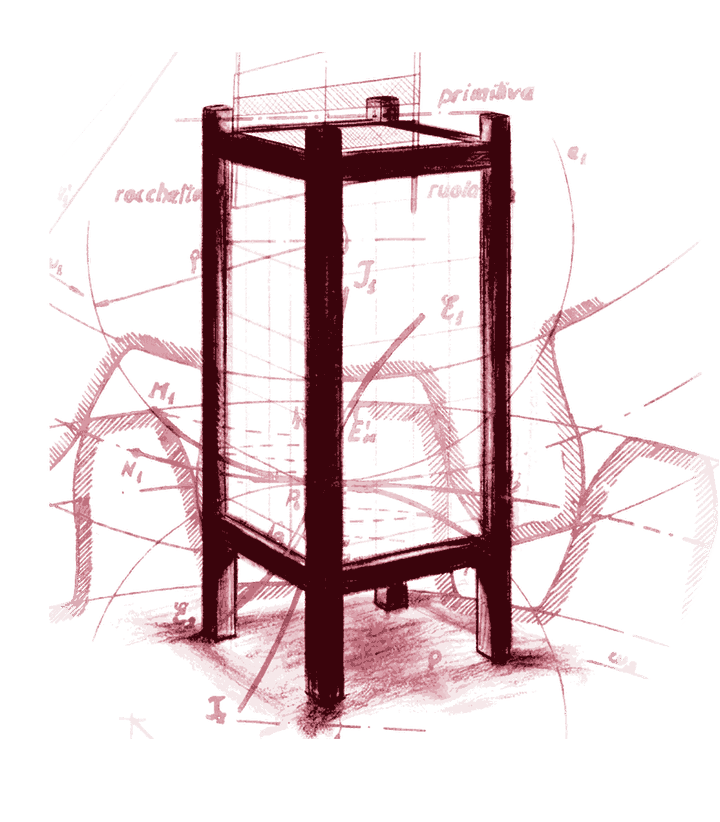
An andon lantern drawn in pencil over a technical drawing of gear wheels.
ANDONThe signal that stops the line
Why this symbol

It is a Japanese andon lantern, drawn over the construction drawing of a gear wheel taken from an old applied mechanics course. I wanted to keep the two together because, in my experience at least, the light is there to see the problem and the drawing is there to solve it, and neither is enough on its own.

The inefficiencies that cost the most are the ones people have got used to.

A machine breakdown is noticed at once and somebody deals with it. The losses that weigh most over time are different: the ones an organisation has stopped noticing because "it's always been done this way", that cost a little every day and rarely show up in a report. The ones I have come across most often are six, and you'll find them below.

Anomalies that come back

The same defect comes back every quarter and is contained each time, while the root cause stays open. The cost ends up in warranty and with the customer.

Scattered information

The fix for a failure often exists already, but it sits in an email, in a file on someone's desktop or in the memory of a technician close to retirement, and the people who need it can't find it.

Manual processes dressed up as digital

Spreadsheets passed from hand to hand, double data entry, figures realigned once a month. The ERP is there, but a good part of the work happens outside it.

Reactive quality

The problem surfaces when the customer complains, and at that point quality becomes an office that chases problems instead of a function that prevents them.

Tools nobody uses

Software designed by people who have never worked on an assembly line, at a test bench or in a service workshop. It is often very complete and very expensive, and for that very reason little used.

Decisions without data

Priorities are set in meetings, often by whoever speaks loudest. The data exists, but it doesn't reach the table where decisions are made in time.

Signals on: 0 of 6 On a production line, when something goes wrong, the operator pulls the cord or presses the andon button and the team leader steps in. In offices and support functions an equivalent signal is usually missing, or it's there and nobody looks at it.

A name for a way of working.

AndonLab is the name I gave to my professional philosophy and to this space, where I collect what I have learned and what I am building. The two words stand for the two halves of the same job.

Andon

Making the problem visible

In Lean Production the andon is the device that flags an anomaly on the line straight away. Behind it there is a clear organisational choice: the people working on the product have the right, and the responsibility, to stop the process when quality or safety is at risk.

Stopping costs money, and that is why many companies end up switching the signal off or not looking at it. From what I have seen, though, an hour of stopped line almost always costs less than a defect that reaches the customer and stays in warranty for years.

Lab

Building the answer and testing it

Once the problem has been seen, you need a place to build an answer and try it out in the field. In my case it brings together industrial experience, direct observation of processes, data and digital tools.

I am interested in small, verifiable solutions that someone can start using within a few days and whose effect can be measured in the weeks that follow. Platforms that need months of configuration before they deliver a result are something else, and that is not what I am trying to do.

In practice it means finding what slows the work down, creates waste or undermines quality, and turning experience into solutions, organisational or digital, that the company is then able to keep going.

Thirty years in industry, from the plants to leading complex organisations.

Iveco / CNH Industrial, about 18 years
SDF, 2015–2026
Board
1995Degree, La Sapienza
1997Daily line, Suzzara
2000Valladolid, Spain
2005Eurocargo
2008Lyon, Irisbus
2011IDV, Magirus
2013Lyon, Bus
2015SDF, Quality
2021–2024SDF Group Board, COO from 2023
2025–2026Vitibot, then AndonLab

I have worked both in the plants, close to the assembly line, the test bench and the service workshop, and at headquarters, with management responsibilities up to the Board of Directors. Having gone through the company's functions let me understand where problems form and how to solve them.

The customer as the reference point

In my work I have always tried to point the organisation's activities towards customers and their satisfaction. I have dealt with very different customers: tradespeople who use commercial vehicles for their work, municipal operators running public transport for their communities, farmers, and armies from half of Europe on peacekeeping missions around the world.

THE STAGES

The beginnings, at Iveco and in Spain1997–2005 · from the Daily line in Suzzara to the one in Valladolid

I started in 1997 at Iveco in Suzzara, on the Daily assembly line, as production line manager; then I moved to shop-floor quality and product quality. In December 2000 I moved to Valladolid, first as Plant Quality Manager and then as head of the body-in-white shop, and I stayed there for more than four years. That is where I learned to work in a plant and an industrial culture different from my own.

Iveco and CNH Industrial2005–2015 · Eurocargo, a year running Irisbus, Defence, Bus again

From 2005 to 2008 I was responsible for product quality on the Eurocargo range.

From 2008 to 2011 I worked in Lyon, at Irisbus, heading Customer Satisfaction & Quality, which brought quality and technical service together on a European scale. For about a year the company had no business leader, and together with the heads of the other departments we ran Irisbus, in effect a company within the company, largely on our own, with a monthly review directly with Iveco's CEO, who had taken on the role ad interim. It was a big step in my professional growth and a life experience I remember with great pleasure.

From 2011 to 2013 I led product quality at Iveco Defence Vehicles. During that time I was able to talk with the people who used IDV vehicles in the theatres of peacekeeping missions. It was an eye-opening experience, and what stayed with me most is the meaning and the value of reliability in that kind of mission.

From 2013 to 2015 I went back to Lyon, for product quality across the whole Bus Product Line.

SDF, up to the Board of Directors2015–2026 · quality, reliability, reorganisation, Board and COO

From June 2015 to March 2026 I worked at SDF, Same Deutz-Fahr, a family-owned multinational that designs and builds tractors and agricultural machinery. I joined in Quality and over the years held roles of growing responsibility: from 2021 to 2024 I was a member of the group's Board of Directors and, between 2023 and 2024, Chief Operating Officer; I was also joint Managing Director of SDF Italia SpA.

They were more than ten years in which I led the work on product quality and reliability and, with responsibilities that kept widening, the evolution of the organisation and its processes, including their digitalisation. Together with the teams I led we achieved significant results in product reliability, warranty costs, technical service levels, industrial efficiency, and the development and industrialisation of new products.

Vitibot, in Reims2025 · general management of a scale-up

In 2025 I took on the general management of Vitibot SA in Reims, France, a company part-owned by SDF that develops fully electric autonomous robots for vineyards. It is a small, technologically advanced business with the typical problems of a scale-up: very different from a structured group, and for that very reason it taught me a great deal.

What I learned first-hand

I have almost always worked on technologically complex products, with a large number of components and a high level of innovation, used in the most varied conditions. Over time I learned that experience is a solid foundation, but that stepping only slightly outside familiar patterns is enough for it to fall short. It is expertise itself that tells you where a rigorous process is needed and where the know-how you have built up is already enough.

More than once I worked with first-rate suppliers who discovered the limits of their own standards starting from a failure on products I was responsible for. Their expertise was real, but it had been built on different operating conditions, and getting to the cause meant questioning even what had seemed settled.

I have seen production plans that started out as challenging turn out, along the way, to be unrealistic. When nobody says so in time, the bill arrives all at once: first in the plant, then at the customer. Checking a plan's assumptions at the start costs far less than catching up afterwards.

And I have seen the opposite outcome too: problems to fix on machines already delivered which, tackled together with the service network, ended up strengthening the relationship with customers instead of damaging it. Consistency and reliability are the basic ingredients of a relationship of trust, and trust is one of the key elements of customer satisfaction.

People

Of the things I have done over these years, one I paid most attention to is the growth of the people who worked with me. I tried to build responsibility and skills inside the teams, so that they would not depend on me, because that is what stays in the company when a manager leaves.

What I bring with me

First of all, a trait I care a lot about: the ability to settle into the new environments I find myself working in and to listen without prejudice. It served me abroad, in Spain and France, and again in 2015, when I moved from a listed group to a family-owned multinational with a very different company culture. I always start from respect for what is already there, which often has an important history behind it that made it what it is today, and I want to understand before I give my view. Then, when a decision has to be made, I make it firmly, with full knowledge of the facts.

Then the ability to look at an industrial company as a single system, in which product development, production, supply chain, quality and technical service depend on one another and have to be managed together, with the customer as the common reference point. I learned it in large international groups and in a scale-up, going from the assembly line to the operational management of a group and to its Board of Directors. These are levels at which the horizon of decisions changes a great deal, and at each of them I tried to turn strategic choices into organisation and processes that people could sustain.

This path also gave me a method: connect the problem in the field, the process that generates it, the data that describes it and the decision that solves or postpones it, and measure every improvement with an indicator agreed before starting. I apply it in the same way to a recurring defect and to the reorganisation of a function.

The results of these years were achieved together with the teams I led: no industrial indicator moves thanks to one person alone. The specific figures belong to the companies I worked for and stay with them; if you are interested, I am happy to talk about them in person, within the limits of what I can say.
How I work, in four steps.

These are the steps I usually follow, in the same order. There is nothing original about them: it is how you work when, in the end, someone has to answer for the result.

1OBSERVE

Look at the problem where it happens

In the plant, in the workshop or in the engineering office, talking with the people who do the work, before proposing any solution.

2CLARIFY

Define priorities and requirements

Decide what has to be solved now, what can wait and what is better left alone, in a short list shared with the people who decide.

3DESIGN

Build a workable solution

A solution that the people and the existing systems can sustain. If the organisation can't carry it, even the best one on paper won't last.

4MEASURE

Check and consolidate

An indicator agreed before starting and checked afterwards, and a proper handover, because the result has to hold even when the person who started it is no longer there.

Where artificial intelligence can help, and where it can't.

I think that every now and then you should take the time to look at things from the outside, with a little distance. I have done so, with the aim of understanding which of the operational problems I know well can be tackled better with today's digital tools, and which will keep needing mainly people, process and discipline. Digitalising processes, after all, has been a constant part of my work in recent years.

The areas I know best

  • Product and process quality: field claims, warranty, root causes
  • Operations and supply chain: inventory, S&OP, plant flows
  • Product development and new model launches
  • Technical service and the service network
  • Organisation of technical functions and change management

These are the fields in which I feel able to tell a real problem from one that only looks like one.

What I am trying to do

I am learning to build web and mobile applications to test a hypothesis: that the most useful tools are the ones designed by people who know the process, more than the ones with the most features.

It is work in progress. The things that work I publish in the Lab.

NOTE

I see AI as one of the tools I have available: it makes sense to use it when it makes people more effective in their work or makes information easier to find. If a problem can be solved with a clear procedure and a spreadsheet, that remains the right answer. In my experience the hard part is knowing precisely what the tool has to do, and to know that you need to have done that job.

The Lab: where I try to build tools.

For now the Lab mostly holds exercises on topics of general interest, which I used to learn how to develop applications, from the simplest ones to more demanding projects. The tools tied to my own trade will go there, starting with an analysis of warranty claims that is under construction now.

4 exercises published 1 tool in progress 5 ideas on the parts list
Go to the Lab

If something you have read here reminded you of a problem you know, I'd be glad to talk about it.

I am interested in exchanging views with people who work every day on industrial processes, quality, technical service or supply chain, about concrete problems, experiences or ideas for tools to build. I reply personally.

From early 2027 AndonLab will also become a professional activity. I will work alongside industrial companies on quality, operations and technical service, through consulting or management assignments; when it is the right answer, also with digital tools built around their processes.

If you are considering this kind of support for next year, we can start talking about it now.

alessandro@andonlab.com
LinkedIn Italiano, English, Español, Français

This site collects no data, uses no cookies and does not track visits. If you write to me, your email stays between you and me.

TitleAlessandro LucianiANDONLAB
Drawn byA. Luciani
PlaceTurin
Revision09 / 2026
Next revision01 / 2027
Data collectedNone
Sheet1 of 2
© 2026 Alessandro Luciani. Personal website with no commercial purpose.No cookies, no tracking.